When a defect appears on the shop floor, the immediate response is usually clear.
Separate the affected product. Inspect the remaining quantity. Decide whether the material can be reworked, downgraded or must be scrapped. Protect the customer and restore production.
These actions are necessary.
But they answer only the first question:
What should we do with the defective product?
The more important question is:
What is the process trying to tell us?
A defect is not only an unsuccessful unit. It is evidence that something in the operating system has moved away from the expected condition.
If the organization removes the product but ignores the signal, it may have contained the incident without correcting the process.
The visible defect may have an invisible history
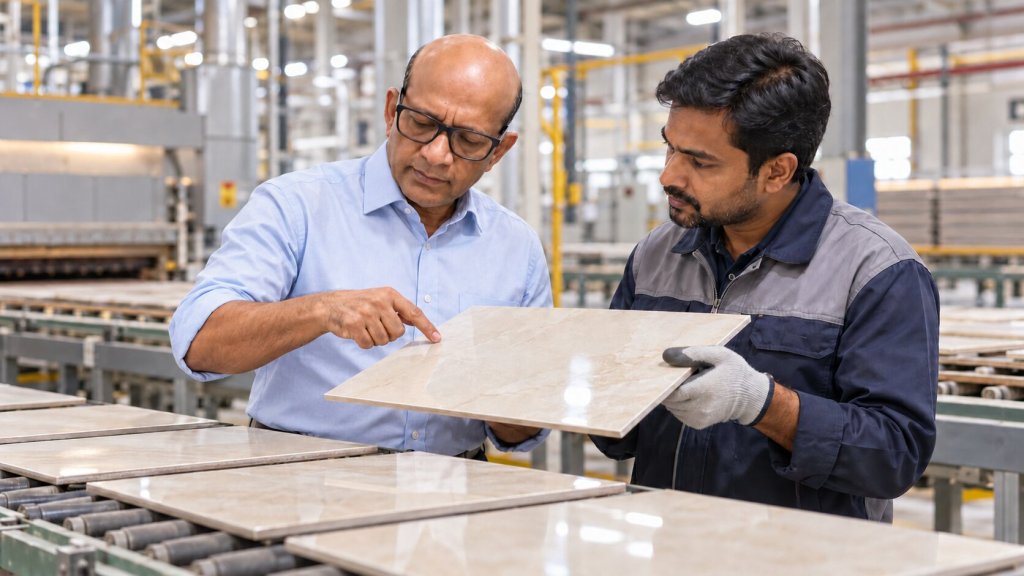
In ceramic manufacturing, a defect visible on a finished tile may have developed much earlier.
The cause might relate to raw-material variation, moisture, forming pressure, drying conditions, glazing, kiln performance or material handling. The point at which the defect becomes visible may not be the point at which it was created.
This is what makes root-cause analysis difficult.
The finished product carries the result of many previous process steps. By the time the problem reaches inspection, the original operating condition may have changed and additional material may already be moving through production.
The organization therefore needs more than the rejected unit.
It needs the history surrounding that unit.
Containment is not corrective action
Containment protects the immediate operation.
It may include:
- Isolating affected material
- Increasing inspection
- Stopping further processing
- Adjusting production settings
- Informing downstream teams
- Protecting customer deliveries
- Reworking or replacing the product
These actions reduce exposure. They are often urgent and necessary.
But containment does not prove that the cause has been eliminated.
If production resumes after an adjustment without determining why the deviation occurred, the organization remains dependent on inspection and intervention.
The same defect may return under a different batch, shift, product or operating condition.
Closing the immediate incident can create the appearance of resolution while the process remains vulnerable.
Repetition changes the meaning of an exception
The first occurrence may reasonably be treated as an isolated event.
The second should increase curiosity.
When the same defect continues to appear, it is no longer sufficient to process each occurrence as a separate quality event.
Repetition suggests that the organization may be managing the output while leaving the underlying condition unchanged.
A recurring problem should prompt questions such as:
- Is the defect linked to a particular material or supplier batch?
- Does it occur on a specific line, tool or work center?
- Is it associated with a product family or operating range?
- Does it appear after a changeover or maintenance activity?
- Are process settings being adjusted consistently?
- Is the inspection method identifying the problem reliably?
- Was the previous corrective action implemented and verified?
These questions move the discussion from product disposition to process learning.
Root cause rarely belongs to one department
A quality defect may appear during production, but its cause can cross several functions.
Procurement may own the supplier relationship. Production may control process settings. Maintenance may understand equipment condition. Engineering may define operating parameters. Quality may own inspection and corrective-action methods. Planning may determine sequence and campaign length.
This means quality improvement cannot be delegated entirely to the quality department.
The team that detects the problem may not control the condition that created it.
Effective resolution requires a clear owner and coordinated investigation across the relevant functions.
Without this ownership, each team may complete its own activity while the end-to-end problem remains.
SAP can provide traceability—but not automatic learning
SAP can connect quality results with materials, batches, suppliers, production orders, equipment, work centers and inventory status.
This traceability is valuable.
It helps the organization identify what was produced, which inputs were used, where the material moved and which decisions were recorded.
But recording a defect is not the same as learning from it.
A quality notification can be created and closed while the same problem continues. A usage decision can correctly block material without removing the cause. A corrective-action field can be completed without later verifying whether performance improved.
The system can preserve the evidence.
The organization must still turn that evidence into a decision and sustained action.
The language of quality data matters
Patterns become difficult to identify when similar defects are described differently.
One person may record “surface mark.” Another may write “visual variation.” A third may enter free text that describes the same condition in different words.
Each record may be understandable individually. Collectively, however, the data may not reveal that the organization is experiencing one recurring problem.
Useful quality data requires practical discipline:
- Consistent defect categories
- Clear severity definitions
- Accurate material and batch references
- Relevant process and equipment context
- Timely recording
- Named corrective-action ownership
- Target completion dates
- Verification of effectiveness
The purpose is not to collect more data.
It is to collect enough consistent context to support learning.
AI can help find the pattern
Business AI can strengthen quality management by examining combinations that people may not easily connect.
It may identify that a defect is more frequent with a particular material source, production sequence, operating condition or equipment history. It may summarize recurring notifications or highlight corrective actions that have not reduced recurrence.
That can help teams investigate faster.
But AI cannot compensate for missing context, inconsistent classifications or corrective actions that were never verified.
It can find patterns in the information available to it.
The organization still needs to determine whether the pattern is meaningful, decide what action to take and confirm that the action worked.
AI can accelerate investigation.
It does not remove accountability.
Close the learning loop
A quality issue should not be considered complete merely because the affected material has been dispositioned or the notification has been closed.
The stronger test is whether the process became more reliable.
That requires checking later performance:
- Did the defect recur?
- Did its frequency decline?
- Was the corrective action fully implemented?
- Did the action create an unintended consequence elsewhere?
- Should the operating standard or control plan change?
- Can the learning be applied to other products or locations?
This final verification converts corrective action from an administrative task into operational improvement.
Listen to what the process is saying
No operation eliminates every defect.
The important difference is how the organization responds when one appears.
A weak response removes the defective unit and returns to production.
A stronger response contains the risk, preserves the evidence, identifies the cause, assigns ownership and verifies improvement.
The defect then becomes more than a cost.
It becomes information that helps the organization understand its process more clearly.
A defect is not just scrap. Properly examined, it is a message from the process—and an opportunity to make the operation more dependableWhen a defect appears on the shop floor, the immediate response is usually clear.
Separate the affected product. Inspect the remaining quantity. Decide whether the material can be reworked, downgraded or must be scrapped. Protect the customer and restore production.
These actions are necessary.
But they answer only the first question:
What should we do with the defective product?
The more important question is:
What is the process trying to tell us?
A defect is not only an unsuccessful unit. It is evidence that something in the operating system has moved away from the expected condition.
If the organization removes the product but ignores the signal, it may have contained the incident without correcting the process.
The visible defect may have an invisible history
In ceramic manufacturing, a defect visible on a finished tile may have developed much earlier.
The cause might relate to raw-material variation, moisture, forming pressure, drying conditions, glazing, kiln performance or material handling. The point at which the defect becomes visible may not be the point at which it was created.
This is what makes root-cause analysis difficult.
The finished product carries the result of many previous process steps. By the time the problem reaches inspection, the original operating condition may have changed and additional material may already be moving through production.
The organization therefore needs more than the rejected unit.
It needs the history surrounding that unit.
Containment is not corrective action
Containment protects the immediate operation.
It may include:
- Isolating affected material
- Increasing inspection
- Stopping further processing
- Adjusting production settings
- Informing downstream teams
- Protecting customer deliveries
- Reworking or replacing the product
These actions reduce exposure. They are often urgent and necessary.
But containment does not prove that the cause has been eliminated.
If production resumes after an adjustment without determining why the deviation occurred, the organization remains dependent on inspection and intervention.
The same defect may return under a different batch, shift, product or operating condition.
Closing the immediate incident can create the appearance of resolution while the process remains vulnerable.
Repetition changes the meaning of an exception
The first occurrence may reasonably be treated as an isolated event.
The second should increase curiosity.
When the same defect continues to appear, it is no longer sufficient to process each occurrence as a separate quality event.
Repetition suggests that the organization may be managing the output while leaving the underlying condition unchanged.
A recurring problem should prompt questions such as:
- Is the defect linked to a particular material or supplier batch?
- Does it occur on a specific line, tool or work center?
- Is it associated with a product family or operating range?
- Does it appear after a changeover or maintenance activity?
- Are process settings being adjusted consistently?
- Is the inspection method identifying the problem reliably?
- Was the previous corrective action implemented and verified?
These questions move the discussion from product disposition to process learning.
Root cause rarely belongs to one department
A quality defect may appear during production, but its cause can cross several functions.
Procurement may own the supplier relationship. Production may control process settings. Maintenance may understand equipment condition. Engineering may define operating parameters. Quality may own inspection and corrective-action methods. Planning may determine sequence and campaign length.
This means quality improvement cannot be delegated entirely to the quality department.
The team that detects the problem may not control the condition that created it.
Effective resolution requires a clear owner and coordinated investigation across the relevant functions.
Without this ownership, each team may complete its own activity while the end-to-end problem remains.
SAP can provide traceability—but not automatic learning
SAP can connect quality results with materials, batches, suppliers, production orders, equipment, work centers and inventory status.
This traceability is valuable.
It helps the organization identify what was produced, which inputs were used, where the material moved and which decisions were recorded.
But recording a defect is not the same as learning from it.
A quality notification can be created and closed while the same problem continues. A usage decision can correctly block material without removing the cause. A corrective-action field can be completed without later verifying whether performance improved.
The system can preserve the evidence.
The organization must still turn that evidence into a decision and sustained action.
The language of quality data matters
Patterns become difficult to identify when similar defects are described differently.
One person may record “surface mark.” Another may write “visual variation.” A third may enter free text that describes the same condition in different words.
Each record may be understandable individually. Collectively, however, the data may not reveal that the organization is experiencing one recurring problem.
Useful quality data requires practical discipline:
- Consistent defect categories
- Clear severity definitions
- Accurate material and batch references
- Relevant process and equipment context
- Timely recording
- Named corrective-action ownership
- Target completion dates
- Verification of effectiveness
The purpose is not to collect more data.
It is to collect enough consistent context to support learning.
AI can help find the pattern
Business AI can strengthen quality management by examining combinations that people may not easily connect.
It may identify that a defect is more frequent with a particular material source, production sequence, operating condition or equipment history. It may summarize recurring notifications or highlight corrective actions that have not reduced recurrence.
That can help teams investigate faster.
But AI cannot compensate for missing context, inconsistent classifications or corrective actions that were never verified.
It can find patterns in the information available to it.
The organization still needs to determine whether the pattern is meaningful, decide what action to take and confirm that the action worked.
AI can accelerate investigation.
It does not remove accountability.
Close the learning loop
A quality issue should not be considered complete merely because the affected material has been dispositioned or the notification has been closed.
The stronger test is whether the process became more reliable.
That requires checking later performance:
- Did the defect recur?
- Did its frequency decline?
- Was the corrective action fully implemented?
- Did the action create an unintended consequence elsewhere?
- Should the operating standard or control plan change?
- Can the learning be applied to other products or locations?
This final verification converts corrective action from an administrative task into operational improvement.
Listen to what the process is saying
No operation eliminates every defect.
The important difference is how the organization responds when one appears.
A weak response removes the defective unit and returns to production.
A stronger response contains the risk, preserves the evidence, identifies the cause, assigns ownership and verifies improvement.
The defect then becomes more than a cost.
It becomes information that helps the organization understand its process more clearly.
A defect is not just scrap. Properly examined, it is a message from the process—and an opportunity to make the operation more dependable

