One of the earliest lessons I learned in manufacturing was that a production plan can look excellent on paper and still be difficult to execute on the shop floor.
The required quantities are clear. The machines appear to have sufficient capacity. Materials are expected to be available. The schedule fits neatly within the available working hours.
Then production begins.
A critical material arrives late. A machine runs below its assumed speed. A quality problem places inventory on hold. A changeover requires more time than expected. The right people are not available on the required shift. An urgent customer order changes the sequence.
The plan has not necessarily failed because people executed it poorly.
It may have failed because the assumptions behind it did not reflect operating reality.
This leads to an important lesson:
A production plan is only as good as the constraints it recognizes.
Every plan contains assumptions
A production plan is more than a list of quantities and dates. It is built on assumptions about how the operation will perform.
These assumptions may include:
- Machine availability and operating speed
- Labor and skill availability
- Material availability
- Production yields
- Changeover duration
- Quality-release time
- Maintenance requirements
- Storage and material-handling capacity
- Supplier reliability
- Transportation lead times
When these conditions are accurately represented, the plan provides useful direction.
When they are missing, outdated or overly optimistic, the plan may create the appearance of control without providing a realistic path to execution.
The problem is not always visible immediately. The schedule may still be released. Production orders may still be created. Materials may still be allocated.
The gaps appear later—through rescheduling, expediting, overtime, manual intervention and missed commitments.
The shop floor reveals what the planning model missed
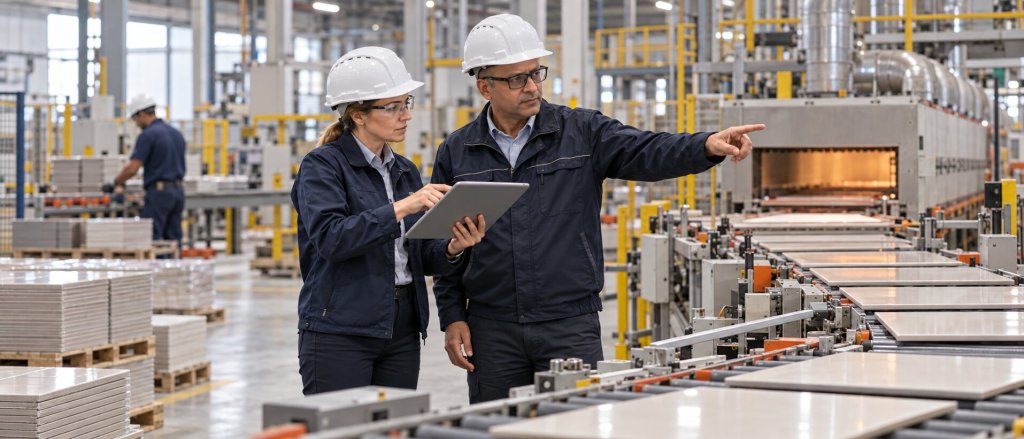
The shop floor is where planning assumptions meet physical reality.
A planning system may treat two machines as having similar capacity, while experienced operators know that one performs differently for a particular product. A standard changeover time may be technically correct but unrealistic when additional cleaning or quality checks are required.
Material may appear available in the system while being held for inspection, assigned to another priority or physically located where it cannot be used immediately.
These are not merely execution problems. They are signals that the planning model and the operating environment are no longer fully aligned.
This distinction matters.
If every deviation is treated as a one-time exception, teams will repeatedly repair schedules without improving the assumptions that created the problem.
A mature operation asks a second question:
What did this exception teach us about the way we plan?
SAP can calculate only with the information it receives
SAP can bring discipline, integration and visibility to production planning. It can connect demand, inventory, procurement, manufacturing and customer commitments across the enterprise.
But the quality of the resulting plan depends on the information and rules within the system.
If lead times are outdated, capacity is overstated or production versions do not reflect actual operating choices, the system will calculate from those assumptions.
The calculation may be technically correct while the result remains operationally unrealistic.
This is why planning accuracy is not solely an IT responsibility.
It requires ongoing participation from production, maintenance, quality, supply chain, procurement and master-data owners. These teams understand the constraints that affect daily execution and must help ensure that the planning model continues to reflect them.
An integrated system does not eliminate the need for operational knowledge.
It makes the quality of that knowledge more consequential.
Not every constraint belongs in the system
It is also important to remain practical.
No planning model can represent every condition that may arise on the shop floor. Trying to configure every possible exception can make the solution unnecessarily complicated and difficult to maintain.
The objective is not to create a perfect digital copy of every operating detail.
The objective is to identify the constraints that materially affect decisions and commitments.
A useful planning model should answer questions such as:
- Which resources genuinely limit output?
- Which materials create the greatest supply risk?
- Which changeovers materially affect available capacity?
- Which quality or regulatory steps cannot be compressed?
- Which assumptions frequently cause rescheduling?
- Which exceptions require human judgment?
Some variability should remain under the control of experienced planners and production teams. But recurring, material constraints should not remain permanently outside the planning model.
When the same workaround is needed repeatedly, it is no longer an exception. It is evidence that the process or its underlying assumptions require attention.
The plan and the floor need a feedback loop
Effective planning is not a one-directional process in which the system sends a schedule to the factory and the factory is expected to follow it.
The shop floor must also send learning back into the planning process.
Actual cycle times, yields, changeovers, shortages, delays and recurring interruptions can reveal where assumptions need to be revised. Planner overrides can also be valuable information when organizations examine why they occurred.
A healthy feedback loop asks:
- Where did execution differ from the plan?
- Was the difference temporary or recurring?
- Did the plan overlook a genuine constraint?
- Is master data still accurate?
- Does the process need to change?
- Should the planning rule change?
- Who owns the corrective action?
Without this discipline, the organization may continually regenerate plans while carrying the same weaknesses forward.
AI does not remove physical constraints
Business AI can help organizations identify patterns, recognize risks and evaluate alternatives faster.
It may detect that a material shortage is likely, predict that a resource will become overloaded or recommend a different production sequence.
These capabilities can improve planning responsiveness.
But AI cannot create physical capacity that does not exist. It cannot make unavailable material appear, eliminate a mandatory quality step or remove the need for a difficult changeover.
Its recommendations will also depend on the reliability of the data, assumptions and business rules available to it.
This makes operational grounding even more important.
The value of AI in planning will not come simply from producing more recommendations. It will come from helping people make better decisions within real operating constraints.
A realistic plan creates trust
When production plans repeatedly ignore shop-floor conditions, people gradually lose confidence in them.
Planners begin maintaining offline spreadsheets. Supervisors create their own schedules. Production teams rely on informal priorities. Customer-service teams seek separate commitments.
Each workaround may solve an immediate problem, but collectively they weaken the integrated planning process.
A realistic plan creates a different response.
People may still need to manage exceptions, but they begin from a shared and credible operating picture. Discussions focus on genuine trade-offs rather than explaining why the plan could never have worked.
That credibility is essential.
The purpose of planning is not to produce a technically complete schedule.
It is to create a plan that the organization can understand, commit to and execute.
Plan for the operation that exists
Every organization wants an ambitious plan. Ambition is necessary for improvement.
But ambition should not be confused with ignoring constraints.
A strong plan makes limitations visible, clarifies trade-offs and helps leaders decide where capacity, process, data or capability must improve.
The shop floor should not merely receive the plan. It should help keep the plan grounded in reality.
SAP can integrate the enterprise. Advanced planning can evaluate alternatives. AI can identify patterns and recommend actions.
But dependable execution still begins with an honest understanding of the operation.
The best production plan is not the one that looks most efficient in the system. It is the one the business can execute—and learn from.


Leave a Reply